The Price Step between Four Layers and Six
Moving from four to six layers adds 30 to 55 percent to bare board cost through double core usage, lamination press overhead, and tighter registration yields.
Moving from four to six layers adds 30 to 55 percent to bare board cost through double core usage, lamination press overhead, and tighter registration yields.

Multilayer PCB fabrication laminates etched copper cores and prepreg under heat and vacuum, creating vertical interconnects through precision drilling and copper electroplating.

Stackup selection balances resin flow, z-axis dielectric constants, and panel utilization to fix bare-board cost, impedance tolerances, and factory pool.
In-situ quasi-optical interferometry resolves thermo-mechanical dielectric tensor degradation across sequential reflow passes, preventing mmWave phase error.

Mid-loss laminates paired with low-roughness copper foil match high-cost ultra-low-loss performance at a fraction of the raw panel price.

Quantifying stacked microvia thermal fatigue requires matching resin z-axis CTE limits to electrodeposited copper ductility under continuous resistance monitoring.
Heat-cured epoxies achieve superior strain transfer efficiency and lower creep drift than cyanoacrylates under high temperatures and long-term static loads.

Sequential lamination registration budgets require root-sum-square alignment modeling of sub-core thermal shrinkage and drill offsets to size microvia lands.

Selecting selective soldering tooling shields requires matching composite thermal resistivity against component clearance gaps to guarantee zero thermal damage.

Correlating micro-ohmic resistance drift in thermal stress coupons with microsection defect rates isolates latent inner layer post separation before assembly.

High-frequency laminate rheology dictates prepreg flow kinetics, fixing pressed dielectric thickness, local impedance stability, and panel registration yield.

Subassembly press hydraulic parallelism and thermal ramp control determine resin distribution, eliminating dielectric height variation and differential signal phase skew.

Latent microvia interfacial fatigue opens during thermal transients to cause intermittent high-speed signal failures detectable only by dynamic four-wire thermal screening.
Volume PCB shops hold a real-world minimum annular ring of 0.002 inches for Class 2 designs when artwork grants 0.005 inches of nominal land margin over tool size.

Sequential lamination registration drift requires statistical bivariate vector modeling to size microvia capture pads for multi-pass ultra-high-density core panels.

Mid-loss laminates optimize high-speed signal reach between 5 and 28 Gbps by controlling dielectric loss without imposing low-loss fluoropolymer costs.

Substrate dielectric drift alters high-frequency signal phase velocity and impedance under thermal stress, requiring flat TCDk resin selection to hold timing margins.
Selecting dielectric substrates requires balancing dissipation factor, glass weave uniformity, foil roughness, and panel yields to meet high-speed impedance targets.
Stackup thickness control requires calculating pressed prepreg heights over local copper patterns to hold impedance and microvia drilling tolerances.

Continuous high-speed Kelvin monitoring during rapid thermal cycling isolates latent target pad separations that re-nest and pass static ambient tests.

Predict anisotropic deformation in sequential lamination by coupling layer-specific thermal expansion tensors with non-linear viscoelastic resin cure shrinkage.
IPC-4101 slash sheets establish mandatory baseline physical, thermal, and electrical limits that override generic trade names to enforce material reliability.
Lead-free reflow shifts substrate permittivity by altering free volume and desorbing moisture, changing line impedance by up to 2.5 ohms on high-speed traces.

Silica-filled resin viscosity minimization requires synchronizing heating ramps with press pressure timing to ensure complete void encapsulation without core shift.
Substrate thermal distortion shifts surface features out of optical focal planes, causing false inspection calls that demand dynamic surface mesh compensation.
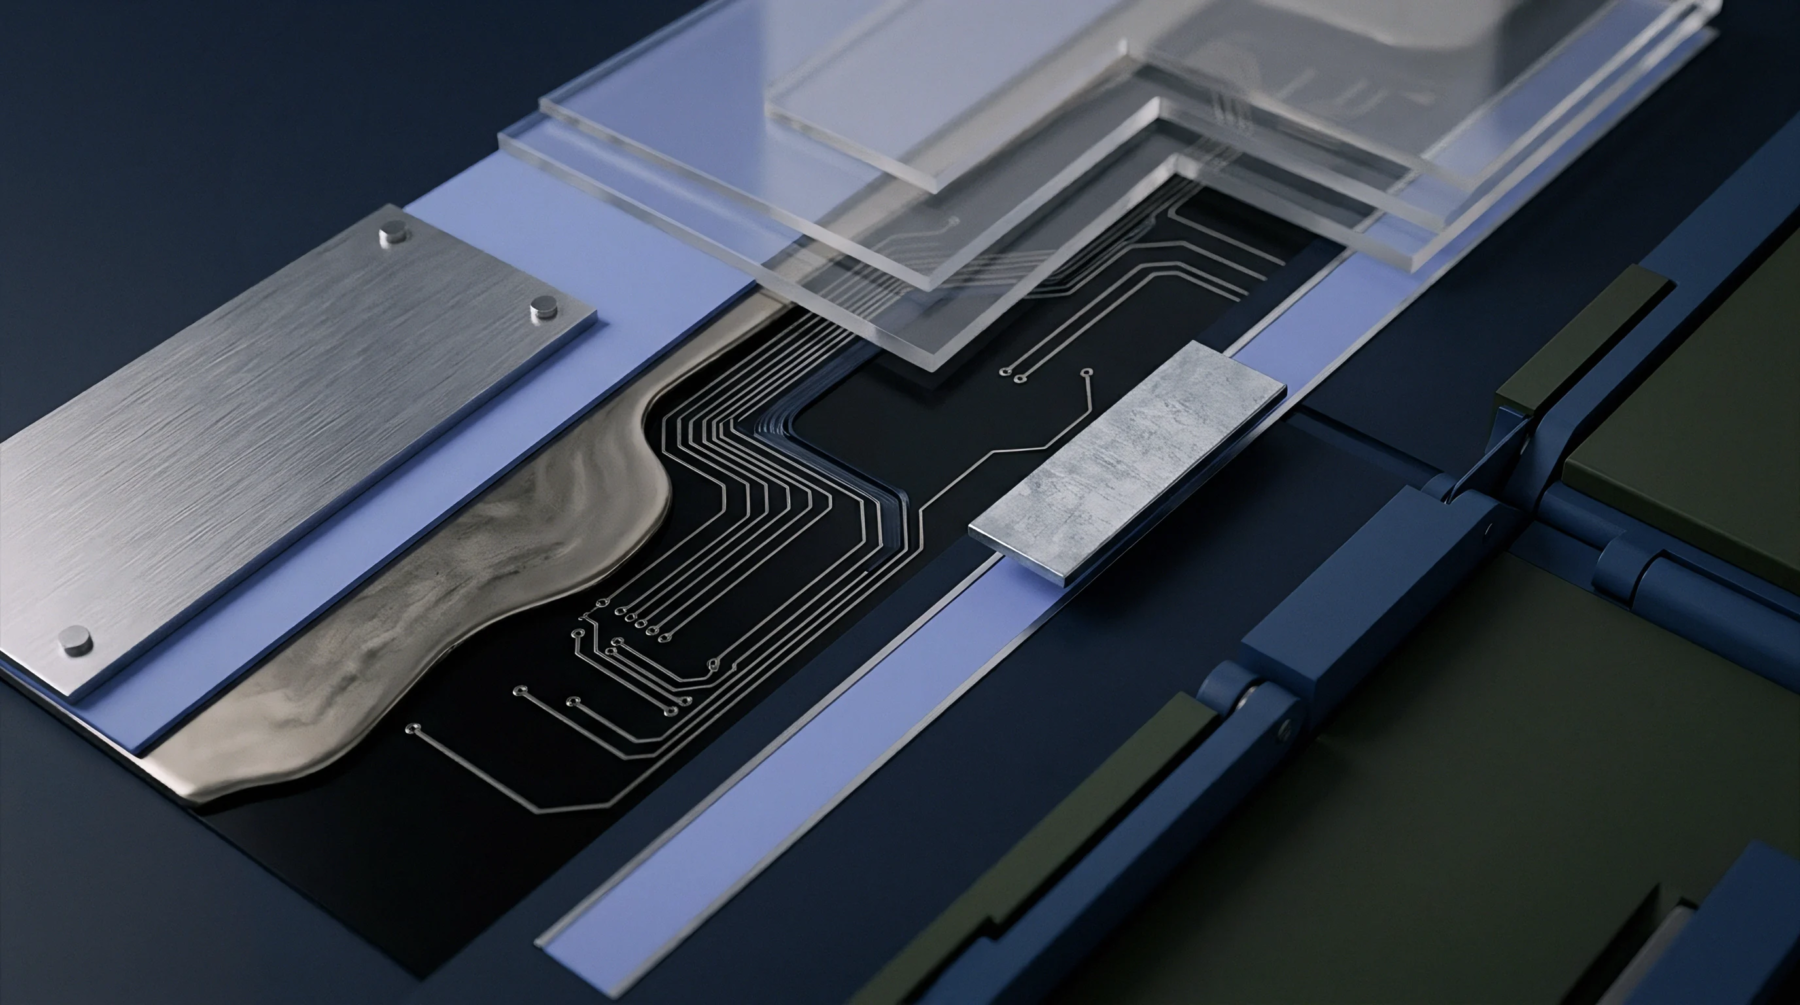
Controlling lamination thermal ramps between 1.5 and 2.0 °C per minute minimizes resin stress and phase skew in sequential multilayer stackups.

Non-linear platen thermal modeling eliminates extended panel registration drift by applying dynamic, localized vector scaling during laser direct imaging.
Sub-millimeter spatial dielectric variations from glass weaves and filler distribution shift dynamically under heat, requiring spread glass and low TCDk resins.

Verification of thermal rework degradation limits relies on coupon continuous resistance tracking and microsectioning to prevent latent inner-layer via cracking.
Low z-CTE silica-filled laminates (IPC-4101/129) and staggered microvia topologies prevent target pad separation during 260°C lead-free reflow excursions.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.