The Price Step between Four Layers and Six
Moving from four to six layers adds 30 to 55 percent to bare board cost through double core usage, lamination press overhead, and tighter registration yields.
Moving from four to six layers adds 30 to 55 percent to bare board cost through double core usage, lamination press overhead, and tighter registration yields.

Multilayer PCB fabrication laminates etched copper cores and prepreg under heat and vacuum, creating vertical interconnects through precision drilling and copper electroplating.

Specifying staggered microvias and single-press HDI stackups preserves multi-vendor competition while cutting panel scrap costs.
Dynamic resin flow in thin core laminates governs post-press dielectric thickness, feature filling capability, and panel impedance uniformity.

Sub-hundred-micron fine-line multi-core panel surcharges stem from seed-etch yield hits, core-shift registration buffers, and panel margin expansion.

Spread glass weaves minimize micro-spatial permittivity variations, stabilizing high-frequency phase delay when press thermal cycles are tightly controlled.
Sub-30 µm dielectric void suppression requires matching non-Newtonian dynamic viscosity to vacuum press ramps to maintain shear flow prior to cross-linking gelation.
Sub-sixty micron trace fabrication mandates semi-additive processing over subtractive etching to eliminate undercut and hold tight differential impedance.

Off-axis artwork rotation increases gross panel utilization on paper but degrades true net commercial yield through anisotropic lamination twist and registration scrap.

Quantifying stacked microvia thermal fatigue requires matching resin z-axis CTE limits to electrodeposited copper ductility under continuous resistance monitoring.

Sequential lamination registration budgets require root-sum-square alignment modeling of sub-core thermal shrinkage and drill offsets to size microvia lands.

Non-Newtonian resin flow inside thin prepreg micro-channels governs void formation, trace displacement, and dielectric thickness stability during high-pressure lamination.
Viscoelastic boundary slip and capillary pressure dictate microvia filling and trace stability during high-density circuit board lamination.

Unambiguous contract allocation caps assembly liability at process fees while tying thermal damage claims to independent coupon microsectioning evidence.
Correlating micro-ohmic resistance drift in thermal stress coupons with microsection defect rates isolates latent inner layer post separation before assembly.

High-frequency laminate rheology dictates prepreg flow kinetics, fixing pressed dielectric thickness, local impedance stability, and panel registration yield.

Multilayer PCB lamination relies on managing dynamic resin viscosity and glass fabric permeability to fill copper features without starving dielectric layers.
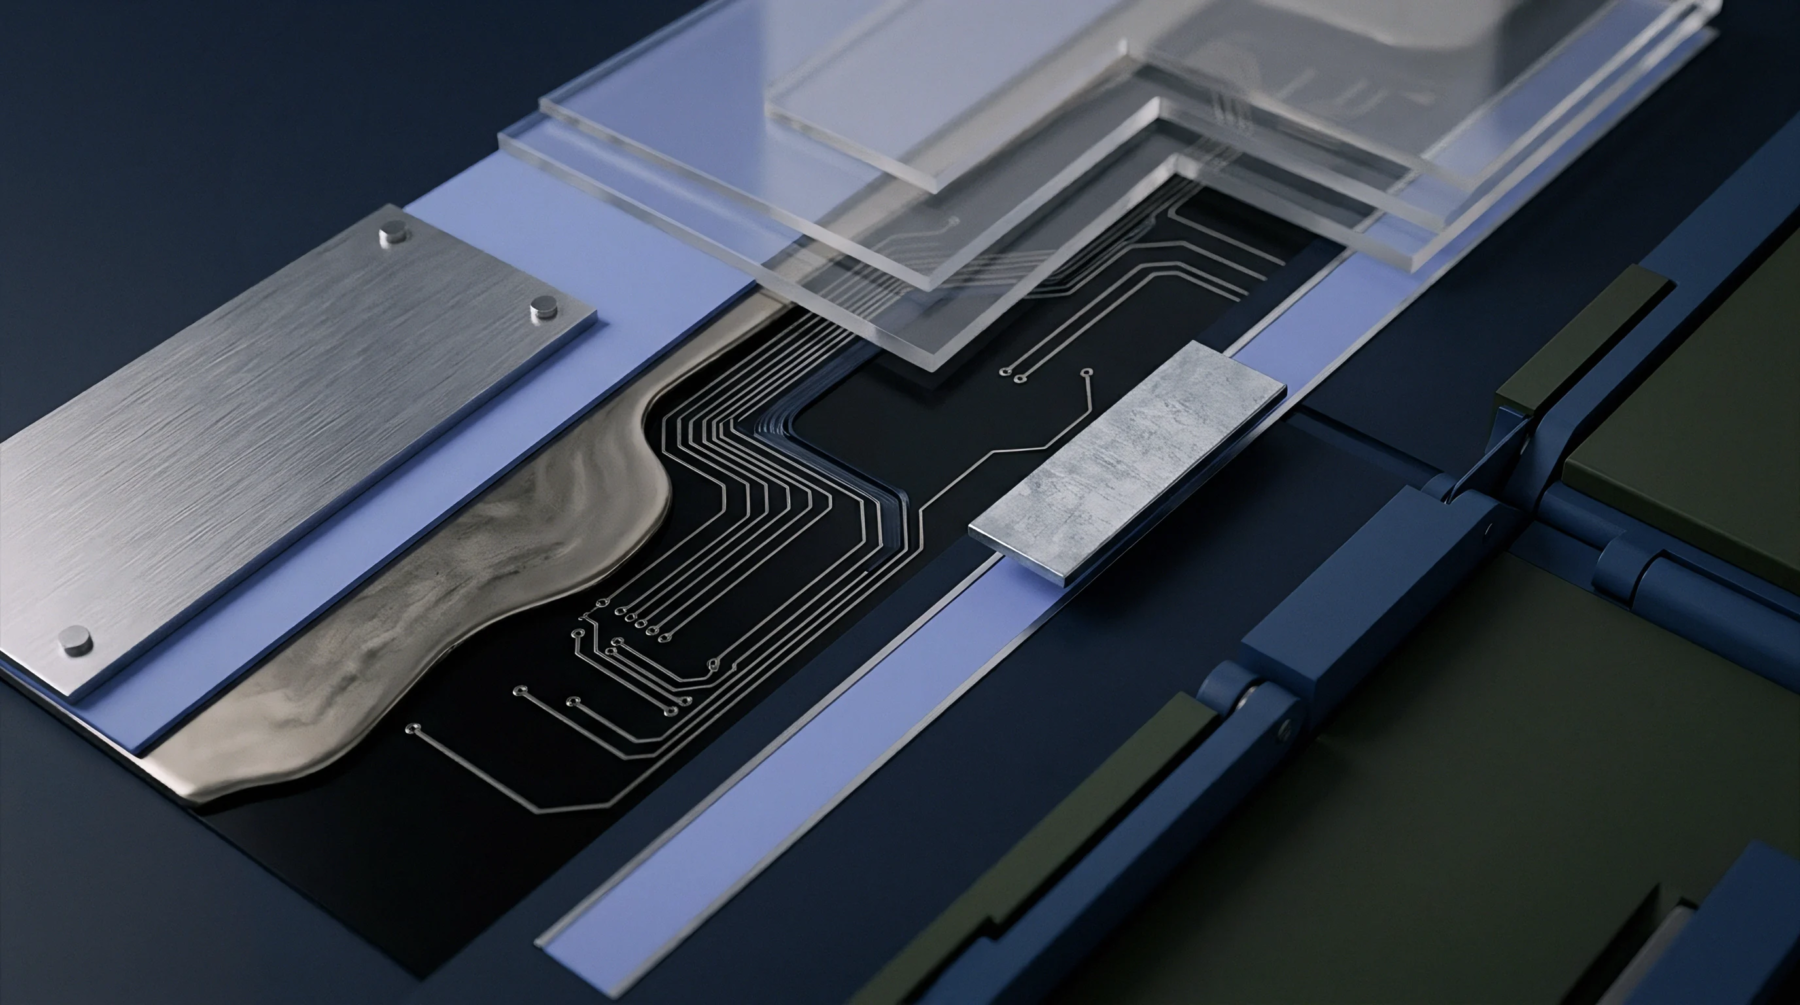
Shear forces during vacuum pressing shift heavy copper traces when resin flow velocity exceeds interfacial bond strength, requiring optimized aspect ratios.

Subassembly press hydraulic parallelism and thermal ramp control determine resin distribution, eliminating dielectric height variation and differential signal phase skew.
Multilayer directional permittivity variance causes stripline capacitance shifts that must be corrected by modeling in-plane and out-of-plane dielectric constants separately.

Latent microvia interfacial fatigue opens during thermal transients to cause intermittent high-speed signal failures detectable only by dynamic four-wire thermal screening.

Stitching via arrays and eddy current losses damp cavity resonances to suppress power plane noise in high-speed substrates.

Unscreened high-frequency channel structural escapes drive PCI Express residual bit error rates above spec limits by inducing localized signal resonances.

Modified semi additive process contracts require clear yield baselines, defect attribution formulas, and flash-etch metrology to recover scrap costs cleanly.

Sequential lamination registration drift requires statistical bivariate vector modeling to size microvia capture pads for multi-pass ultra-high-density core panels.
Sub-50µm trace etching requires migrating from subtractive foil etching to mSAP or A-SAP seed layers, paired with ISO Class 5 cleanroom photolithography.
Calibrating optical inspection on sub-30 µm traces requires 3D slope profiling artifacts to prevent false line-width scrap driven by sidewall taper shift.
Spatial resin gradients in heterogeneous cores alter localized permittivity, requiring spread-glass selection and off-axis trace routing to control high-frequency phase skew.

Microstructural recrystallization and impurity segregation drive grain boundary shear failure at microvia target pad interfaces during high-temperature reflow.
Sub-stack thickness drift stems from secondary resin compression during sequential lamination, requiring flow-controlled prepregs and thieving arrays to hold Z-axis impedance.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.